As Amazon Associates, we earn from qualifying purchases. This means we may receive a small commission at no extra cost to you if you click through and make a purchase.
Recommended Print Speed
600 mm/s
Build Volume
260 x 260 x 260 mm³
Product Dimensions
17.93"D x 17.93"W x 18.16"H
Total Machine Weight
13.6 kg
Full spec sheet 6 more rows from the listing
| Maximum Hotend Temperature | 300℃ |
| Pre-Installed Nozzle | 0.4 mm hardened steel |
| Supported Nozzle Sizes | 0.25 mm, 0.6 mm, 0.8 mm |
| Filament Drying Capability | Integrated ACE 2 Pro with 65℃ active heating |
| Standard Material Capacity | 4 colors (expandable to 8 colors with 2 units) |
| Frame Construction Material | Metal |
Shoppers evaluating whether the Anycubic Kobra 3 Combo fits their workshop need to weigh its high-speed multi-material capabilities against the realities of mechanical maintenance. Multi-color 3D printing has transitioned from a niche modification to an accessible production standard, and this platform tackles multi-filament management by bundling an open-format bed-slinger with an active four-spool dry box. Buyers can expect rapid motion capabilities, rigid metal components, and integrated thermal filament conditioning directly out of the box. However, running an open-chassis machine at elevated speeds while cycling multiple automated feeds creates distinct physical demands that warrant careful inspection before purchase.
This reliability audit examines the anycubic kobra 3 combo specs to determine how its components hold up across sustained production schedules. We explore core anycubic kobra 3 combo reliability, potential feeding bottlenecks inside the anycubic kobra 3 combo ace pro material box, frame behavior during rapid directional shifts, routine anycubic kobra 3 combo maintenance tasks, and common anycubic kobra 3 combo issues such as tube friction and filament jams. Finally, we review expectations surrounding anycubic kobra 3 combo warranty support when wear parts or electronic components need replacement.
What You Get With the Anycubic Kobra 3 Combo


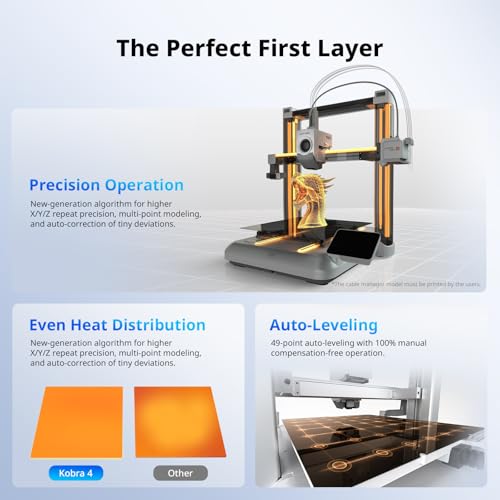
The standard retail package bundles the main motion chassis alongside dedicated external filament conditioning hardware designed to automate multi-color feeding.
- Metal open-frame 3D printer with a 260x260x260mm³ build volume
- ACE 2 Pro filament management system featuring 65℃ active drying technology
- Four-color printing support standard out of the box
- Hardened steel 0.4mm nozzle pre-installed for wear resistance
- High-temperature hotend capable of reaching up to 300℃
- Printhead drive assembly engineered for recommended speeds up to 600mm/s
- Open architecture frame design offering 360-degree print visibility
Hardware Durability and the Open Frame Architecture
The mechanical foundation of the machine relies on an all-metal chassis with an overall weight of 13.6 kg, anchoring the motion system against rapid directional inertia. Pushing printhead travel toward the recommended 600mm/s velocity introduces substantial kinetic forces across both the vertical gantry and the horizontal carriage. The weight of the metal frame provides vital grounding, mitigating harmonic vibrations that would otherwise create ringing or surface banding on tall prints. In contrast to enclosed multi-material platforms like the anycubic kobra s1, this unit maintains an entirely open structural layout, prioritizing quick physical access to the print bed and toolhead.
Operating an open-chassis printer creates specific environmental trade-offs. The listing highlights an accessible open design offering a 360-degree unobstructed view of the print bed, allowing users to detect first-layer lifting or nozzle buildup immediately. This level of visibility removes the visual obstructions common to enclosed machines, simplifying bed leveling checks and build surface cleaning. However, an unenclosed 260x260x260mm³ build envelope leaves active prints exposed to ambient air drafts and room temperature shifts. While standard materials like PLA or PETG print reliably in open air, draft-sensitive materials face heightened delamination risks without supplemental enclosure protection.
Kinetic longevity across moving parts demands consistent oversight when operating at high velocities. Accelerating a toolhead to 600mm/s generates rapid friction along rolling guide surfaces, requiring regular lubrication and periodic belt tension adjustments. The metal frame prevents structural warping over continuous hours of operation, but users must treat mechanical fastening checks as a regular responsibility. If structural bolts loosen under sustained vibration, dimensional tolerances drop noticeably, highlighting the importance of inspecting frame fasteners between heavy production runs.
Material Routing and Active Drying Performance
Multi-filament management centers on the ACE 2 Pro unit, which merges automated material switching with active thermal conditioning. Moisture absorption represents a primary cause of stringing, rough exterior layers, and feed clogs in modern desktop printing. The 65℃ active drying technology inside the material box directly tackles this issue by blowing continuous heated air around stored spools during operation. Driving ambient humidity out of moisture-sensitive spools before the filament reaches the extruder significantly lowers bubbling in the melt zone, producing cleaner outer layer finishes during anycubic kobra 3 combo multicolor printing.
Executing seamless color transitions requires precise coordination between the feeder motors and the toolhead extruder. During each color change, the filament must retract several inches back through long PTFE feeder tubes before the next line feeds forward into the melt zone. This continuous cycling creates friction throughout the entire routing line. For users considering an upgrade from single-material machines like the anycubic kobra 3 max combo, managing multiple filament lines requires constant attention to spool winding neatness, tube curvature, and feeder drive tension.
System modularity allows users to expand their color palette beyond the standard configuration. While one ACE 2 Pro box provides four-color printing standard, linking two units together increases capability to eight colors. The manufacturer notes that eight-color expansion operates strictly with ACE 2 Pro boxes, meaning third-party splitters or mismatched hardware cannot integrate with the internal control protocol. Routing eight independent lines introduces additional friction points, requiring smooth tube placement to ensure the feeder motors push filament reliably without grinding or stalling.
Initial Setup Routine and Calibration Demands
A successful anycubic kobra 3 combo setup begins with structured assembly and systematic mechanical alignment before running high-speed prints. Unboxing the 13.6 kg metal machine involves securing the vertical frame uprights, mounting the heated bed, and attaching the multi-wire toolhead harness. The open architecture provides clear tool clearance when tightening bolts and connecting the external dry box. Taking extra care during frame assembly ensures that the vertical gantry rests square against the base, preventing tilt that could degrade bed leveling accuracy across the 260x260mm build plate.
Integrating the ACE 2 Pro unit requires careful management of the PTFE feed tubes to avoid feeding resistance. The tubing connecting the dry box to the toolhead must be routed in gentle arcs rather than tight bends. Sharp bends force the internal feeder motors to work against severe mechanical drag, which can trigger false runout warnings or ground-down filament. Users familiar with basic multi-color setups like the anycubic cobra x will appreciate the built-in drying system, but they must still route filament paths cleanly to prevent mechanical feed errors.
Automated calibration routines represent the final preparatory phase before starting production. Running the machine at up to 600mm/s requires accurate sensor-based bed leveling and resonance testing to compensate for rapid toolhead movements. Allowing the printer to run its complete calibration sequence establishes precise Z-offset values and maps bed unevenness. Rushing past these automated setup routines can cause nozzle contact with the build plate or uneven extrusion widths, creating avoidable first-layer defects that derail early print attempts.
Preventive Maintenance and Wear Management
Maintaining reliable anycubic kobra 3 combo reliability over continuous printing cycles depends on an active maintenance schedule. Multi-color printing demands hundreds of automated retractions and reloads during a single job, speeding up mechanical wear on drive gears and nozzles. The pre-installed 0.4mm hardened steel nozzle provides superior wear resistance compared to standard brass nozzles when feeding abrasive materials. The toolhead also supports interchangeable nozzles in 0.25mm, 0.6mm, and 0.8mm diameters, allowing users to adjust layer detail or volumetric flow according to their project needs.
Preventing an anycubic kobra 3 combo clogged nozzle requires disciplined thermal oversight during material transitions. When switching between filaments with varying melting temperatures, residual plastic in the hotend melt pool can scorch or solidify if transition temperatures are set incorrectly. Although the 300℃ hotend easily handles high-temperature filaments, running standard PLA immediately after high-temp plastics can cause partial jams inside the heat break. Performing routine cold pulls and using cleaning filaments between material transitions keeps the melt channel clear of debris.
Regular anycubic kobra 3 combo maintenance must cover motion hardware alongside the toolhead. Drive belts must be inspected every few weeks, as rapid 600mm/s velocity shifts naturally stretch rubber belts over extended use. Linear rods and guide tracks need regular cleaning to remove airborne dust before re-applying light lubrication. Inside the ACE 2 Pro box, the 65℃ active heating element and drive gears should be checked periodically to clear out stray filament fragments or dust that can collect inside the drive mechanisms.
Anycubic Kobra 3 Combo Pros and Cons
Pros
- Integrated ACE 2 Pro with 65℃ active filament drying
- Durable 300℃ hardened steel nozzle included standard
- Expandable multi-material printing up to eight colors
- Recommended print speeds reaching up to 600mm/s
- Sturdy 13.6 kg all-metal chassis
Cons
- Open frame provides no ambient thermal draft protection
- Eight-color printing requires purchasing a second material box
- Multi-filament tube routing requires careful manual clearance
Is the Anycubic Kobra 3 Combo Worth It
Evaluating whether the anycubic kobra 3 combo is worth it comes down to your production priorities and comfort with multi-material mechanics. For creators wanting an accessible entry into multi-color printing, this bundle offers a capable balance of motion speed, all-metal construction, and integrated filament conditioning. The 65℃ active drying feature within the ACE 2 Pro eliminates the frustration of printing with moisture-laden spools without requiring external dehydrating ovens. Makers producing multi-tone prototypes, educational displays, or detailed decorative prints will find the four-color standard setup highly capable.
However, users focused on printing high-temperature technical plastics such as nylon or polycarbonate will face clear constraints with this platform. The open frame lacks thermal retention, meaning large-scale parts printed with shrinkage-prone materials remain vulnerable to corner warping and layer splitting. If your workflow centers on structural mechanical brackets rather than decorative multi-material designs, an enclosed single-filament printer may offer more consistent thermal conditions for demanding engineering polymers.
For hobbyists, design studios, and small print shops needing versatile multi-color production, the system delivers practical utility. The inclusion of a 300℃ hardened steel nozzle, flexible nozzle sizes from 0.25mm to 0.8mm, and high print speeds make it a versatile manufacturing tool. As long as you maintain proper belt tension, route your feed tubes cleanly, and perform regular nozzle care, this bundle provides dependable multi-material output without occupying excessive bench space.
FAQ
How does the ACE 2 Pro active drying feature work?
The ACE 2 Pro utilizes 65℃ active heating technology to circulate warm air around spools inside the closed chamber. This continuous heat evaporates ambient moisture from filament strands during storage and active printing. Removing moisture prevents steam bubbling, nozzle spitting, and surface blemishes on finished models.
Can the printer handle abrasive filaments straight out of the box?
Yes, the unit comes equipped with a 0.4mm hardened steel nozzle rated for temperatures up to 300℃. Hardened steel resists physical wear far better than traditional brass, allowing users to print abrasive materials without rapidly eroding the nozzle bore, though the open frame remains best suited for filaments that tolerate ambient room conditions.
What causes an Anycubic Kobra 3 Combo clogged nozzle during color changes?
Clogged nozzles during multi-color printing typically stem from temperature mismatches between swapping filaments or excessive friction during rapid retractions. If residual high-temperature filament stays inside the melt zone while lower-temperature filament feeds in, partial blockages can form. Using cleaning filament and running proper purge volumes prevents these jams.
How do you expand the system to print with eight colors?
Expanding to eight colors requires purchasing and connecting a second ACE 2 Pro unit. The manufacturer specifications state that eight-color operation functions exclusively with up to two ACE 2 Pro boxes linked together. Third-party multi-material accessories cannot integrate with the printer’s native multi-color control interface.
What should buyers know about Anycubic Kobra 3 Combo warranty support?
Buyers evaluating warranty support should distinguish between structural hardware and routine consumable parts. While the metal chassis, motherboard, and heating electronics are covered under standard manufacturer warranty terms, high-friction items like nozzles, PTFE tubes, and extruder gears are treated as normal wear items. Contacting official support promptly with photographic evidence ensures faster resolution for manufacturing defects.